Structural Steel Pre-Shipment Inspection Checklist for Overseas Buyers
For international contractors, developers, and procurement managers, purchasing fabricated structural steel from China involves more than comparing prices and confirming delivery schedules.
Before structural steel components leave the fabrication factory, buyers need to verify that the products, inspection records, and shipping preparations meet the agreed project requirements.
Problems involving fabrication dimensions, welding quality, protective coatings, missing components, or incomplete documentation can result in additional costs and installation delays after the materials arrive overseas.
A well-planned pre-shipment inspection helps buyers identify outstanding issues before transportation and provides an opportunity to resolve them while the components remain at the factory.
However, final inspection should not replace quality control activities conducted throughout fabrication.
This structural steel pre-shipment inspection checklist explains what overseas buyers should verify before fabricated components leave the factory, which documents should be reviewed, and how to establish a practical shipment release process.
1. Why Pre-Shipment Inspection Matters
Pre-shipment inspection is an important verification stage in international structural steel procurement.
Its purpose is to confirm that the fabricated products and supporting documents meet the agreed requirements before the steel components are released for transportation.
Identifying Problems Before Overseas Delivery
Once fabricated structural steel has been shipped internationally, correcting quality problems can become significantly more complicated.
For example, an incorrectly positioned connection plate may require modification before the component can be installed.
If the issue is discovered at the fabrication factory, the supplier may be able to correct it before shipment.
If the same problem is discovered at an overseas construction site, the buyer may face additional engineering reviews, transportation costs, installation delays, or repair expenses.
Pre-shipment inspection can help identify visible defects, dimensional discrepancies, missing components, and incomplete delivery documentation before these problems affect site operations.
Final Inspection Cannot Replace In-Process Quality Control
Some structural steel quality requirements cannot be adequately verified through a final visual inspection alone.
For example, welding, nondestructive testing, surface preparation, and coating application may require inspections at specific stages of fabrication.
Once welding is completed or protective coatings have been applied, certain conditions may become difficult to examine without additional work.
Therefore, buyers should distinguish between inspections performed during production and the final verification conducted before shipment.
For projects governed by applicable AISC requirements, quality control and quality assurance responsibilities are addressed through the relevant specifications and project documents.
The inspection scope, acceptance criteria, and responsibilities should be established before fabrication begins.
Establishing Clear Shipment Release Requirements
A pre-shipment inspection should produce more than a simple statement that the steel appears acceptable.
Before authorizing shipment, buyers should confirm that:
- Required fabrication and quality inspections have been completed.
- Inspection reports and relevant material documentation are available.
- Identified nonconformities have been resolved or formally dispositioned by authorized parties.
- Fabricated components and quantities correspond to the agreed supply scope.
- Packaging, identification, and shipping documents are ready for verification.
Depending on the contract, these activities may involve the fabricator’s quality control team, the buyer’s representative, or an appointed independent inspection agency.
Third-party inspection is not automatically mandatory for every structural steel export project. Its necessity and scope depend on applicable requirements and contractual arrangements.
The key takeaway: Pre-shipment inspection should serve as the final verification stage of an established quality management process—not as the first or only opportunity to identify fabrication problems.
2. Verify Drawings, Materials and Dimensions
Before fabricated structural steel is released for shipment, buyers should confirm that the components correspond to the approved fabrication drawings, material specifications, and agreed supply requirements.
This verification is particularly important for international projects, where discovering missing or incorrectly fabricated components after delivery can lead to installation delays and additional costs.
Review Approved Fabrication Drawings
The first step is to confirm which drawings and revisions were used for fabrication.
Structural steel projects may involve design drawings, shop drawings, connection details, and revised technical instructions.
Before shipment, the inspection team should verify that:
- The latest applicable approved fabrication drawings are available.
- Drawing revision numbers match the manufacturing records.
- Approved changes have been incorporated into the relevant components.
- Component identification marks correspond to the drawings and fabrication records.
- Outstanding technical clarifications affecting fabrication have been resolved.
A component should not be accepted solely because it matches an outdated drawing.
If deviations from approved requirements are identified, they should be documented and evaluated through the project’s established approval procedure.
Verify Materials and Identification
The inspection process should also confirm that the supplied materials correspond to the specified steel grades and product requirements.
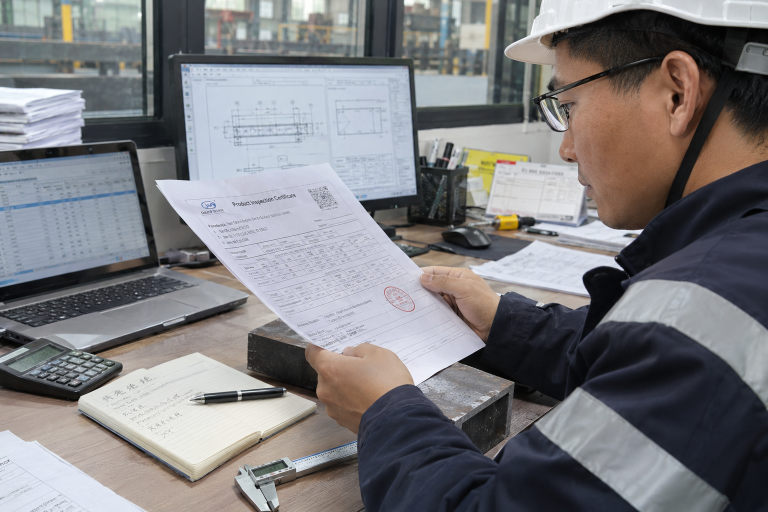
Depending on the project, relevant records may include material test certificates, purchasing documents, material identification records, and inspection reports.
For example, an industrial warehouse may contain structural members manufactured from different steel grades or product specifications.
The inspection team should be able to verify that the correct materials have been used in the relevant components.
Material identification and full material traceability are not necessarily the same requirement.
The level of identification, heat-number tracking, and supporting documentation should follow the applicable standards and contract specifications.
Check Component Dimensions and Connection Details
Dimensional verification is essential for ensuring that fabricated steel components can be assembled and installed according to the approved design.
Typical inspection items include:
- Overall lengths and relevant cross-sectional dimensions
- Column and beam geometry
- Connection plate and stiffener locations
- Bolt hole sizes, spacing, and patterns
- Required camber, straightness, and alignment
- Other project-specific dimensional requirements
For example, a steel beam with incorrectly positioned connection holes may create problems during site assembly.
However, dimensional acceptance should be based on the applicable fabrication tolerances and approved project documents rather than arbitrary limits.
Different fabrication features may be governed by different tolerance requirements.
Measurements should also be recorded using appropriate equipment and procedures.
Confirm Component Quantities and Identification Marks
Structural steel packages may contain hundreds or thousands of individual components.
Before shipment, the supplier should verify that fabricated components correspond to the applicable approved bill of materials, erection drawings, and agreed delivery schedule.
Particular attention should be paid to component identification marks and the quantities assigned to each shipment.
For projects delivered in multiple batches, buyers should confirm which components are included in each shipment and whether the shipment sequence supports the construction schedule.
The inspection process should identify missing components, unexpected duplicates, or discrepancies between fabrication records and the proposed shipping list.
Practical Verification Summary
| Inspection Item | Supporting Evidence |
|---|---|
| Approved drawings and revisions | Approved fabrication drawings and revision records |
| Material specifications | Material certificates and identification records |
| Component dimensions | Dimensional inspection reports |
| Connection details and bolt holes | Approved drawings and inspection results |
| Component identification | Part marks and fabrication records |
| Shipment quantities | Bill of materials and proposed packing list |
These documents should be reviewed together rather than independently.
For example, a component may meet dimensional requirements but still require clarification if its material identification or drawing revision does not match the approved records.
The key takeaway: Before shipment, buyers should verify not only that structural steel components have been manufactured, but also that their materials, dimensions, identification marks, and supporting records correspond to the agreed project requirements.
3. Check Welding and NDT Records
Welding quality is a critical consideration in structural steel fabrication, particularly for load-bearing connections and complex welded assemblies.
Before shipment, overseas buyers should confirm that the required welding inspections have been completed and that the corresponding records are available.
A visual examination of finished components alone may not provide sufficient evidence of compliance with the project’s welding requirements.
Review Welding Procedures and Welder Qualifications
For projects specifying AWS D1.1, structural steel welding should be performed according to that code and the approved project requirements.
Depending on the specified code and welding processes, relevant documentation may include:
- Welding Procedure Specifications (WPS)
- Procedure Qualification Records (PQR), where qualification testing is required
- Welder or welding operator qualification records
- Required welding inspection and production records
A WPS describes the welding procedure and the essential conditions for performing the work.
A PQR documents the results of qualification testing used to support a welding procedure, when required by the applicable code.
Not every WPS requires a separate PQR. For example, AWS D1.1 permits prequalified welding procedures under specified conditions.
Buyers should therefore confirm that the welding procedures and personnel qualifications are suitable for the actual work performed, rather than simply checking whether the supplier possesses a collection of welding certificates.
Verify Visual Welding Inspection Records
Visual Testing (VT) is a fundamental method used to evaluate weld quality.
Depending on the applicable acceptance criteria, visual inspections may identify issues such as:
- Visible cracks
- Undercut
- Overlap
- Surface porosity
- Incorrect weld dimensions
- Other visible welding discontinuities
However, visual inspection cannot reliably detect every internal welding defect.
Inspection reports should identify the inspected work, applicable acceptance criteria, inspection results, and the responsible inspection personnel.
If unacceptable weld conditions are identified, the supplier should document the required corrective actions and subsequent verification.
Review Nondestructive Testing Reports
Nondestructive Testing (NDT) may be required for specified welds depending on the applicable standards, structural details, and project specifications.
Common methods include:
Ultrasonic Testing (UT): Used to detect and evaluate certain internal discontinuities in welds.
Magnetic Particle Testing (MT): Used to detect surface and near-surface discontinuities in suitable ferromagnetic materials.
Visual Testing (VT): Used to examine visible weld surfaces and assess workmanship against applicable criteria.
The required testing methods and examination extent should be determined by the project specifications, applicable code, and inspection plan.
Overseas buyers should not assume that every structural steel project requires 100% UT or MT.
When reviewing NDT reports, buyers should check:
- Which welds or components were examined
- The inspection method and examination extent
- The applicable testing procedure and acceptance criteria
- The inspection results and identified indications
- The qualifications of inspection personnel, where required
- Whether any rejected welds were repaired and re-examined
A report stating that testing was completed is not sufficient if it cannot be associated with the relevant welds or project requirements.
Confirm That Welding Nonconformities Are Closed
If a weld fails to meet the specified acceptance criteria, the issue should be recorded and addressed according to the project’s quality procedures.
Depending on the circumstances, corrective action may involve weld repair, additional inspection, or another formally approved disposition.
Buyers should verify that outstanding welding nonconformities have been resolved or formally accepted by an authorized party before shipment release.
Repair records and required reinspection results should be available where applicable.
Welding Quality Documentation Checklist
| Document or Record | What Buyers Should Verify |
|---|---|
| WPS | Applicable welding procedures are available |
| PQR | Required procedure qualifications are supported by test records |
| Welder qualifications | Welding personnel hold suitable qualifications |
| Visual inspection reports | Required visual inspections have been completed |
| NDT reports | Required methods, coverage, and acceptance criteria were applied |
| Repair and reinspection records | Rejected welds have been properly addressed |
| Nonconformity records | Outstanding issues are closed or formally dispositioned |
The key takeaway: Overseas buyers should verify that welding procedures, personnel qualifications, inspection results, and corrective actions collectively demonstrate compliance with the agreed project requirements before authorizing shipment.
4. Inspect Coatings and Surface Treatment
Protective coatings play an important role in reducing corrosion risks during transportation, storage, and the service life of structural steel.
Depending on the project specifications, fabricated components may receive shop primer, a multi-coat protective paint system, or hot-dip galvanizing.
Before shipment, overseas buyers should verify that the specified corrosion protection system has been applied and that the required inspection records are available.
However, the inspection procedures for painted steel and hot-dip galvanized components are different.
Verify Surface Preparation Records
Proper surface preparation is essential for the performance of protective paint systems.
Before painting, steel surfaces may require cleaning, abrasive blast-cleaning, or other specified preparation methods.
Depending on the project, relevant inspection requirements may include:
- Surface cleanliness and rust removal
- Specified surface preparation grade
- Surface profile or roughness
- Dust and soluble salt contamination, where specified
- Environmental conditions before coating application
For example, a project may specify surface preparation requirements based on ISO 12944-4 before primer application.
Once the steel has been painted, it is generally no longer possible to verify the original blast-cleaned surface through ordinary visual inspection.
Therefore, buyers should review surface preparation inspection records rather than relying solely on the appearance of finished painted components.
Check the Protective Paint System
If structural steel is supplied with a protective paint system, buyers should confirm that the applied coating corresponds to the approved project specification.
The verification may include:
- Approved coating manufacturer and product names
- Required primer, intermediate coat, and topcoat
- Specified number of coats
- Coating application and inspection records
- Required curing or handling conditions
- Areas intentionally left uncoated for subsequent site work
A finished component should not be accepted simply because the paint color appears correct.
Different protective coating systems may have different performance characteristics, application requirements, and intended service environments.
Any proposed changes to the specified coating system should be reviewed and approved through the appropriate project procedure.
Review Dry Film Thickness (DFT) Reports
Dry Film Thickness (DFT) is an important inspection parameter for protective paint systems.
DFT refers to the thickness of a coating after it has dried or cured.
Depending on the project requirements, the supplier may need to provide DFT inspection reports identifying the measured components, inspection areas, results, and applicable acceptance criteria.
When reviewing these records, buyers should confirm that:
- The specified nominal thickness and any applicable limits are identified.
- The measurement procedure is appropriate for the coating system and substrate.
- The required inspection areas and sampling plan have been covered.
- Measurement results meet the applicable acceptance criteria.
- Any rejected areas have been repaired and rechecked.
For coatings applied to roughened steel surfaces, ISO 19840 provides a method for measuring and evaluating DFT under its defined scope.
Buyers should avoid accepting arbitrary thickness readings without considering the required measurement method and acceptance criteria.
Inspect Hot-Dip Galvanized Components
Some structural steel projects specify hot-dip galvanizing instead of, or in addition to, protective painting.
For applicable fabricated iron and steel articles, ISO 1461 provides requirements and test methods for hot-dip galvanized coatings.
Before shipment, buyers may need to verify:
- Applicable galvanizing specification
- Zinc coating thickness inspection results
- General coating coverage and visible condition
- Uncoated or damaged areas requiring repair
- Documented repairs and associated acceptance records
- Component identification and completeness after galvanizing
Buyers should also confirm that galvanizing-related requirements are appropriate for the actual product.
For example, continuously galvanized sheet products and certain fasteners may be governed by different product-specific standards.
Therefore, ISO 1461 should not automatically be applied to every zinc-coated product in a structural steel shipment.
Check Coating Damage Before Packing
Even when coating inspection results are acceptable, finished components may experience damage during handling, temporary storage, or preparation for loading.
Before shipment release, the inspection team should check for visible problems such as:
- Scratches or damaged coating areas
- Exposed steel where coating is required
- Visible coating deterioration or contamination
- Damage around lifting and handling points
- Incomplete coating repairs
- Improper contact or protection between components
Any damage should be evaluated and repaired according to the applicable coating specification and approved repair procedures.
Particular attention should be paid to areas that may become difficult to access once components are bundled or loaded into containers.
Coating and Surface Treatment Checklist
| Inspection Item | Supporting Evidence |
|---|---|
| Surface preparation | Cleaning, blasting, and inspection records |
| Approved paint system | Coating specification and application records |
| Dry film thickness | DFT measurement reports |
| Hot-dip galvanizing | Zinc coating inspection records |
| Coating damage | Final visual inspection and repair records |
| Outstanding defects | Approved corrective action and reinspection records |
The key takeaway: Pre-shipment coating inspection should verify both the visible condition of finished structural steel and the inspection records from earlier surface preparation and coating activities. A good-looking painted or galvanized surface alone does not demonstrate full compliance with the specified corrosion protection requirements.
5. Pre-Shipment Checklist and Shipment Release
Completing fabrication does not automatically mean that structural steel is ready for international shipment.
Before authorizing transportation, overseas buyers should confirm that the required inspections are complete, outstanding quality issues have been properly addressed, and the proposed shipment matches the agreed supply scope.
A structured pre-shipment checklist can help procurement teams avoid overlooking important details during the final delivery stage.
Verify Component Quantities and Shipping Marks
Structural steel shipments often contain numerous individual members, connection plates, and accessories.
For large industrial buildings, materials may be delivered in several batches according to the construction schedule.
Before shipment, buyers should reconcile the proposed packing list with the approved bill of materials, component identification records, and agreed delivery scope.
Important checks include:
- Correct quantities of beams, columns, braces, and other members
- Clear and consistent component identification marks
- Correct allocation of components to each shipment
- Identification of loose connection plates and accessories
- Required structural bolts, nuts, and washers, where included in the supply scope
- Identification of missing, duplicated, or incorrectly listed components
Shipping marks should enable the receiving team to identify the components and locate their corresponding positions in the erection documentation.
Where components are bundled together, the relationship between individual piece marks and bundle identification should remain clear.
Inspect Packaging and Transport Protection
International structural steel shipments may involve factory handling, inland transportation, port operations, ocean freight, and unloading at the destination.
Inadequate packaging can cause coating damage, deformation, lost accessories, or handling difficulties.
The final packaging inspection should consider:
- Suitable support and separation between steel members
- Protection of vulnerable edges, coated surfaces, and connection details
- Secure packaging of bolts, nuts, washers, and small accessories
- Clear package identification and handling information
- Appropriate lifting and loading arrangements
- Measures to reduce movement or damage during transportation
Packaging requirements should reflect component geometry, transportation methods, and contractual responsibilities.
For containerized shipments, buyers should also confirm that the proposed loading arrangement accounts for the container’s applicable weight and dimensional limits and the required cargo securing arrangements.
For oversized or unusually heavy components, transportation planning may require additional coordination with the freight forwarder and relevant service providers.
Review the Final Quality Documentation Package
Before shipment, the buyer should request the quality documents required by the contract and inspection plan.
Depending on the project, the documentation package may include:
- Approved fabrication drawings and revision records
- Material test certificates and required identification or traceability records
- Dimensional inspection reports
- Welding procedure and personnel qualification records
- Visual inspection and required NDT reports
- Surface preparation, painting, or galvanizing inspection records
- Nonconformity reports and corrective action records
- Final inspection reports
- Packing lists and component identification schedules
Not every document will be required for every project.
However, the records should be sufficient to demonstrate compliance with the agreed requirements and should be identifiable with the relevant components or shipment batch.
For projects involving several shipments, buyers should avoid accepting a general project-level inspection summary as the only evidence for a specific delivery.
Confirm Nonconformity Closure
A Nonconformity Report (NCR) is used to document work or materials that do not meet specified requirements.
Before shipment release, buyers should review any outstanding NCRs, inspection comments, and corrective action records affecting the shipment.
Each issue should have a documented status and an appropriate disposition.
Possible dispositions may include repair, replacement, rework, rejection, or acceptance under an authorized concession where permitted.
The supplier should not independently treat an unresolved deviation as acceptable when the contract requires approval from the buyer, engineer, or another authorized party.
If repairs or rework require additional inspections, the corresponding results should be reviewed before the affected components are released.
Practical Pre-Shipment Inspection Checklist
The following checklist provides a starting point for overseas buyers purchasing fabricated structural steel.
| Inspection Area | Evidence to Review | Release Requirement |
|---|---|---|
| Approved drawings | Drawings and revision register | Correct revisions confirmed |
| Material compliance | Material certificates and identification records | Specified materials verified |
| Dimensions | Fabrication inspection reports | Applicable tolerances satisfied |
| Welding and NDT | Required inspection and testing records | Results accepted under project criteria |
| Surface protection | Coating or galvanizing records | Requirements met; defects addressed |
| Component quantities | Bill of materials and packing list | Shipment quantities reconciled |
| Piece identification | Component and package marks | Identification consistent |
| Packaging | Packing inspection and photographs | Agreed protection requirements satisfied |
| Quality deviations | NCRs and corrective action records | Release-blocking issues resolved or authorized |
| Final release | Inspection summary and release authorization | Shipment approved by authorized personnel |
This checklist should be adapted to the contract, project specifications, applicable standards, and agreed Inspection and Test Plan (ITP).
It is not a substitute for the technical acceptance criteria established by the project.
Inspection Completed vs Shipment Released
Consider a hypothetical warehouse project involving several hundred fabricated steel members.
The supplier reports that fabrication and final inspection have been completed.
However, the buyer discovers that several braces listed for the first shipment have not been included in the packing list.
Even if the fabricated components pass their quality inspections, the shipment still requires clarification before release.
The parties may need to confirm whether the missing braces will be added, transferred to an agreed later shipment, or otherwise addressed through an authorized change.
Similarly, an unresolved welding NCR may prevent the affected components from being released until the required corrective action or authorized disposition is complete.
A final inspection report should therefore document not only the inspection findings but also the resulting shipment status.
Possible outcomes may include:
- Released: All applicable release requirements have been satisfied.
- Released with approved conditions: An authorized party has formally accepted clearly defined outstanding actions, where permitted.
- On hold: Required evidence, corrective actions, or approvals remain incomplete.
- Rejected: The affected items do not meet the applicable requirements and cannot be released in their current condition.
The contract and inspection plan should identify who has authority to approve release and whether conditional release is allowed.
The key takeaway: A successful pre-shipment inspection should end with a documented shipment release decision—not merely confirmation that the factory has completed production or that an inspector has visited the site.
6. Final Thoughts: Inspect Before You Ship
Pre-shipment inspection is an important part of managing quality risks when purchasing fabricated structural steel from China.
For overseas buyers, the objective is not simply to confirm that production has finished. It is to establish whether the fabricated components, supporting quality records, and shipping arrangements satisfy the agreed project requirements.
An effective inspection process should connect several essential activities: verifying approved drawings, confirming material compliance, reviewing fabrication and welding records, checking protective coatings, and reconciling component quantities with shipping documentation.
Equally important, outstanding nonconformities must be resolved or formally dispositioned by the appropriate authorized parties before affected components are released.
Build Quality Requirements into the Procurement Process
Reliable quality control begins long before the final inspection.
Buyers should define applicable standards, inspection responsibilities, documentation requirements, and shipment release conditions during the RFQ and contract preparation stages.
Choosing a structural steel fabricator in China should therefore involve more than comparing manufacturing prices. Buyers should also assess the supplier’s technical capabilities, quality management procedures, inspection resources, and ability to provide the required documentation.
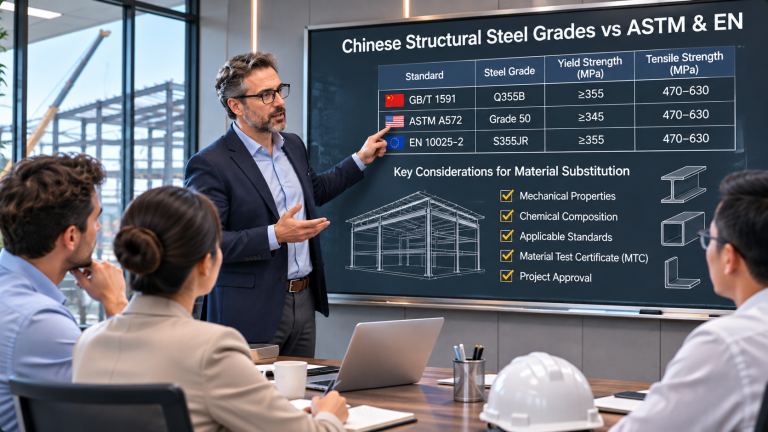
Where international material standards apply, the specified steel grades and any proposed substitutions should be reviewed and approved before procurement and fabrication.
Make Shipment Release a Documented Decision
A pre-shipment inspection report is valuable only when its findings are properly reviewed and addressed.
Before authorizing shipment, the responsible parties should confirm that required inspections are complete, relevant documentation is available, and release-blocking issues have been resolved or formally accepted under the project’s procedures.
For large or phased deliveries, this verification should be performed against the specific components included in each shipment.
A structured checklist helps make the process more consistent, but it should always be adapted to the project’s contractual and technical requirements.
The final takeaway: Inspecting structural steel before shipment is not simply about finding defects. It is about confirming that the products, documents, and delivery arrangements are ready for the next stage of the project.
At SteelSourcing Compass, our goal is to help international buyers make more informed structural steel sourcing decisions through practical procurement guidance, technical insights, and independent industry information.